Description
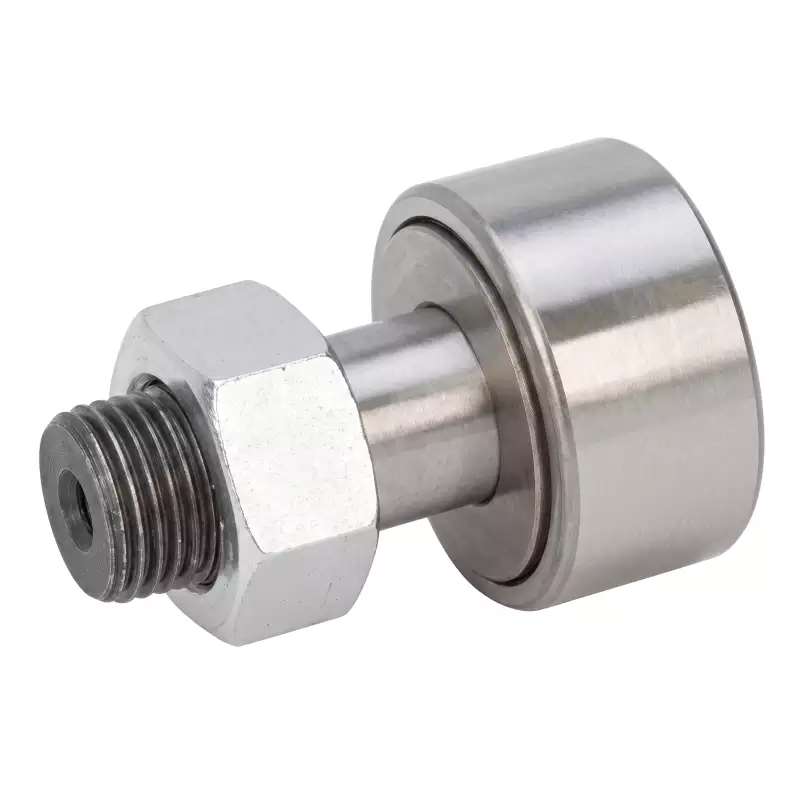
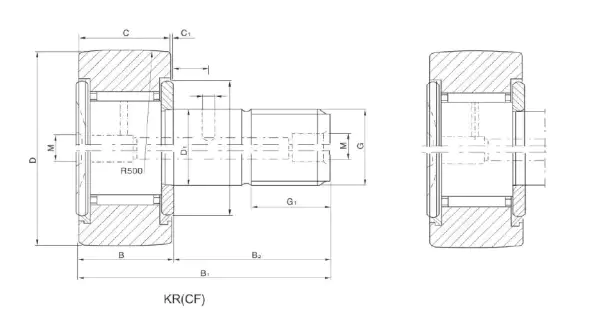
EP-KR22 / EP-KRV22 is the EVER POWER designation for the 22 mm nominal outside-diameter size in the KR/KRV stud type track roller family. It uses a M10x1.25 stud, an outer-ring width of 12 mm and a speed reference of 17,000 rpm. This size is a practical screening point for SMT placement heads, packaging cams, printing mechanisms and textile equipment.
Technical parameters
| Parameter | Value |
|---|---|
| Outside diameter D* | 22 mm |
| Outer-ring width C | 12 mm |
| D1 | 10 mm |
| Stud thread | M10x1.25 |
| Eccentric reference e | 0.3 mm |
| Basic load rating C* | 410 |
| Basic load rating C0* | 320 |
| Speed reference | 17,000 rpm |
| Mass | 44 g |
| IKO reference | CF10 |
| WERB KR legacy | NAKD22 |
| WERB KRV legacy | NAKD22V |
Dimensions and mounting interface
EP-KR22 is the first 22 mm option in the application ranges used across packaging, printing and textile machinery. Speed and repeated-cycle duty should be reviewed together with grease retention and track condition.
| Dimension | Value |
|---|---|
| G1 | 12 mm |
| B max | 13.2 mm |
| B1 max | 36.2 mm |
| B2 | 23 mm |
| B3 | — |
| C1 | 0.6 mm |
| rs min | 0.3 mm |
The M10 mounting interface is compact enough for dense automation, yet the full axial stack still matters. Check shoulder seating, usable stud length and access for the installation tool before treating a matching thread as sufficient.
Construction and configuration choices
The family can use a cylindrical or spherical outer surface depending on design. Confirm the mating-track geometry and edge-contact requirement.
When eccentric adjustment is required, use the KRE / KRVE naming as the enquiry reference and confirm the eccentric value and mounting orientation.
If the mechanism needs a particular KRV sealing arrangement, grease specification, clean-production lubricant or washdown resistance, state it as an ordered requirement.
High-cycle service still requires a clean radial contact path. Check that the cam profile and mounting position do not force the outer ring to act as an axial guide during repeated strokes.
In fast reciprocating equipment, record where the cam transition occurs relative to the contact band. Localized impact at that point can influence service behavior even when the nominal dimensions are correct.
Size-specific selection perspective
Where EP-KR22 / EP-KRV22 fits
This 22 mm size is a common screening point for high-cycle mechanisms such as SMT placement, small packaging cams, printing drives and textile equipment. The M10 stud gives a different mounting interface from the smaller EP-KR19 size even though the overall product still looks compact. When cycle frequency is high, grease retention, temperature rise, track finish and repeated impact become part of the selection conversation. During a retrofit, record both the follower marking and the track width; a correct thread with the wrong outer-ring geometry can still create edge loading. For a new mechanism, leave practical access for tightening and later replacement rather than judging the installation only from the nominal bearing outline.
Use the 22 mm ring and M10 stud as the geometry gate, then review high-cycle motion, impact at cam transitions and grease retention. For SMT or packaging equipment, this keeps replacement identification separate from the operating-duty check.
Replacement and cross-reference identification
IKO CF10 and WERB NAKD22 are useful identifiers for this nominal size. The KRV-family legacy row uses NAKD22V. Use these references to narrow the search, then verify the physical interface and ordered configuration before treating the parts as interchangeable.
| EP reference | IKO reference | WERB legacy | Replacement note |
|---|---|---|---|
| EP-KR22 | CF10 | NAKD22 | Standard KR-family reference; confirm ordered outer-surface and lubrication details. |
| EP-KRV22 | CF10 | NAKD22V | KRV-family reference; confirm sealing/guide configuration for the order. |
| EP-KRE22 / EP-KRVE22 | — | — | Eccentric-family naming when an eccentric arrangement is required; confirm e and the complete interface. |
Selection and installation checks
Confirm D* 22 mm, C 12 mm, M10x1.25 thread, B/B1/B2 geometry and the available shoulder/corner clearance.
Inspect the mating track in the context of high-cycle cam motion. A displaced contact band, ridge or local impact mark can indicate an alignment or track problem that should be corrected before EP-KR22 / EP-KRV22 is installed.
The speed reference is 17,000 rpm. Real operating suitability still depends on load, lubrication, temperature, contamination and cycle pattern.
State KR/KRV/KRE/KRVE preference, outer-surface geometry, lubricant/sealing requirement and any inspection/documentation needs in the RFQ.
Related sizes
Quote EP-KR22 / EP-KRV22 against the real machine interface
Quote this size with the existing marking, quantity, M10 stud engagement, track/cam width, cycle rate and a photo or drawing. For SMT, printing or packaging service, state the contamination and lubrication conditions that influence configuration.